Wednesday, 30 September 2026

Mining Roll Forming Machines: A Buyer's Guide to Specs, Cost, and ROI

Mining sites sit far from the nearest steel service center. A replacement bracket can take six weeks to arrive by road or barge. A fabricator within a day's drive of a mining district turns that wait into same-week delivery, and an on-site roll forming machine removes the road and barge delay entirely.

A mining roll forming machine is a heavy duty line built for thick coil, usually 2.0 to 6.0 mm of high strength steel. It forms conveyor idler frames, stringer channels, structural C and Z sections, ventilation ducting, and cable tray for mine sites. Rate the mill for your thickest coil, not your average, because that is what protects tolerance and output on a mining contract.

The numbers make the case. One conveyor replacement campaign can consume 100,000 meters of stringer channel in a quarter. Roll formed profiles ship as nested bundles, which cuts freight volume 30 to 50 percent.

Mill structure matters. Forming 6 mm high strength steel takes torque a light gauge mill cannot deliver. Heavy duty lines use 60 to 90 mm shafts and gear driven stands rather than chain drives. Stands run from 16 to 26 because thick coil needs gradual bends. Servo inline punching runs 20 to 30 m/min with mounting holes punched in line, so every bracket bolts up without rework.

Coating is a contract item. Cut edge rust on plain galvanized coil in an acidic underground mine appears within two years. Zinc magnesium coil resists cut edge creep far better. Put the coating specification in the contract.

Cost and payback: a single-profile heavy gauge line starts near USD 70,000. A multi-profile automated line with servo punching and stacked bundling exceeds USD 250,000. The payback rests on freight saved on nested bundles, downtime avoided by local stock, and high utilization between mining campaigns.

Read the full article →

Upright Roll Forming Machine Speed: What 3 to 30 m/min Really Means

Most rack-buyer quotes print "25-30 m/min" on the spec sheet. Installed pallet rack upright lines actually run anywhere from 3 to 30 m/min, and one decision drives the entire gap: how the holes get punched. After that decision, upright roll forming machine speed has almost nothing to do with the forming mill itself.

Rack column lines come in three speed classes, set entirely by the punching method. Hydraulic punching stops the strip at every stroke and runs 3 to 4 m/min. A mechanical punch press with clustered dies runs 10 to 15 m/min. Roll punching, where rotary dies punch continuously as the strip travels, reaches 30 m/min and above. Gauge and hole density move you within a class, not between classes. Establish the class first, because every other figure in the quote hangs off it.

The hole math is brutal. On a 2-inch teardrop pitch with both faces punched, every metre of column carries roughly 39 holes. Multiply by line speed and you get the holes per minute the punching system must deliver: about 472 holes/min at 12 m/min. A press with single-hole dies cannot reach that rate, so the line falls back to hydraulic-class pace. The same press with 8-hole cluster tooling needs only 59 strokes per minute to hold 12 m/min. Identical press, identical tonnage, four times the speed, and the offer may not say which tooling is included.

Roll punching removes the stop entirely, the only mechanism that reaches 1,180 holes per minute without stalling or breaking dies. The trade is pattern flexibility: a rotary punch is built for one pattern at one pitch, so it suits long runs of a standard column.

Even with punching solved, the line does not hold nameplate pace all shift. Losses cluster around the same stations: about 13 to 23 percent of the shift produces nothing. The stacker deserves its own warning. It is the cheapest station in the line and the most common cause of lost pace on 9-metre columns. Above 15 m/min the stacker stops being an accessory and becomes the real production limit: at 30 m/min a 9-metre column reaches the exit every 18 seconds, faster than most handling systems can clear a piece.

Daily output for 9m columns follows a simple formula: daily output = effective minutes x line speed / column length. Two shifts multiply the column count by roughly 1.8, because coil changes and die checks take a larger share of a compressed schedule.

Annual output is speed multiplied by available time, and changeover attacks available time directly. A line rated at 15 m/min that needs 6 hours to move from 3-inch to 4-inch columns produces fewer columns per year than a 10 m/min line that changes over in 40 minutes. Modern servo lines treat width and gauge as recipe values, making changeover a software step rather than a manual rebuild.

Read the full article →

Tuesday, 29 September 2026

Agricultural Roll Forming Machines: 7 Farm & Greenhouse Profiles (2026)

Modern farming is a steel business. Commercial greenhouses need steel gutters to carry water away from crops. Vertical farms stack growing channels in steel frames. Livestock barns need roofing that resists ammonia corrosion. Fence posts anchor every perimeter line. Buying these profiles cut to length from a service center works for small projects, but volume buyers lose margin on every meter. An agricultural roll forming machine moves that production in house.

A single line can produce seven farm profiles: cultivation gutters, greenhouse roof arches and ridge caps, C and Z purlins, barn roof and wall cladding, silo stiffener bands, steel fence posts, and hydroponic growing channels.

Speed depends on the profile. Light roof sheets run 25 to 40 m/min. Gutters and structural profiles run 15 to 25 m/min. Heavy silo bands run 10 to 18 m/min. A cassette-style mill swaps between profiles in just 2 to 3 hours, so one line covers gutters up to 4 meters wide and several greenhouse styles.

Material choice decides profile life. Pre-galvanized or zinc-magnesium coil from 0.7 to 1.2 mm, most often Z275 or ZM310, follows the ASTM A653 standard. Greenhouse gutters demand a watertight seam test before shipment, because a leaking gutter destroys crops and trust. Fence posts need a punched hole every 100 mm, so press speed matters as much as forming speed.

Budget benchmarks help planning. A single-profile gutter line starts near USD 40,000. A cassette-based multi-profile line runs USD 80,000 to 150,000. Fully automated lines with servo punching and stacking exceed USD 200,000. Standard configurations ship in 30 to 45 days; custom cassette tooling adds 15 to 20 days. Most lines reach full production within two weeks of arrival.

Believe Industry ships agricultural roll forming lines to 20 plus destination countries, with video-guided installation, remote commissioning, and operator training.

Read the full article →

Wednesday, 23 September 2026

Electrical Roll Forming Machines: Cable Tray & Busway Profiles (2026)

An electrical roll forming machine turns steel coil into the profiles a power distribution network is built from: cable trays, busway enclosures, conduit channels, strut channel, and transformer tank panels. The useful part is that one cassette line can feed a cable tray plant, a switchgear builder, and a transformer workshop from the same coil stock.

Cable tray is the volume product, and it comes in four shapes. Ladder type carries heavy cable runs on two side rails with rungs. Trough type adds a ventilated bottom. Solid bottom (conduit tray) encloses the cable fully. Wire mesh tray is bent from cold drawn wire instead, so it sits outside roll forming. Rails form from 1.5 to 2.5 mm coil, and NEMA Class 20C is the class most export tenders ask for.

Busway and busduct housings route 800 to 6,300 ampere feeders between transformers and main switchgear. The housing clamps around insulated bus bars with fixed clearance, so fold tolerance is tighter than tray work and burr free cutoff is a product requirement rather than a finish detail. Strut channel runs 41 mm with in line perforation, and thin conduit channels form from 0.8 to 1.5 mm coil.

Transformer radiator corrugation is the margin product. Fold depth and pitch are rolled into 1.0 to 1.5 mm cold rolled steel, and the fold depth has to hold within a fraction of a millimeter because it controls radiator surface area.

Two standards decide export eligibility. NEMA VE 1 classes the tray by load and span for North America; IEC 61537 defines the load test most international tenders cite. Coating is settled separately, and coating weight per ASTM A653 belongs in the contract, not in an email thread. Indoor switch rooms manage on Z180 to Z275; coastal and petrochemical sites need 304 stainless.

On line output, punching density matters more than mill speed. NEMA slot patterns put a hole every 50 to 100 mm on a tray rail, so an undersized servo press throttles a mill that can otherwise run 25 m/min.

A single profile tray line starts near 45,000 USD. A cassette based line covering tray, strut, and busway runs 90,000 to 160,000 USD, and fully automated lines with servo punching and stacking pass 200,000 USD.

Read the full article →

Tuesday, 22 September 2026

USA Roll Forming Machine Guide: Power, Steel, Profiles & Landed Cost (2026)

Buying a roll forming machine for the USA market comes down to three hard constraints: ASTM steel grades, 480V three-phase power, and inch-based profiles. Get any one of them wrong and the line will not pass acceptance testing on your floor, no matter how well it ran in the factory.

Power comes first. US industrial supply is 480V, three-phase, 60 Hz, with 110V control circuits. A hydraulic pump motor wound for 50 Hz runs about 20 percent faster on 60 Hz, which changes pump flow, valve response, and flying cutoff tracking. A proper USA-spec build includes 60 Hz rated inverter-duty motors, UL listed wire, and a built-in 480V-to-110V control transformer — not just a wall transformer.

Steel and profiles follow. ASTM A653 Grade 50 galvanized (50 ksi yield) is the workhorse for roofing, purlins, and strut, with ASTM A792 Galvalume for architectural roofing and ASTM A1008 for rack uprights. Standard US master coils come in 24, 36, 48, and 60 inch widths, and 36 inch (914 mm) is the standard feed for panel lines. Profiles are exactly imperial: PBR panels at 36 inch coverage with a 1-1/4 inch purlin bearing leg, strut channel at 1-5/8 x 1-5/8 inch, and C or Z purlins from 6 to 12 inch depth.

On compliance, the machine itself is not certified — the profiles it produces must let roof assemblies pass UL 580 uplift testing and rack members meet ANSI MH16.1, so the tooling must hold print dimensions tightly.

Landed cost is where budgets break. Roll forming machines classify under HTS 8462.21, and Chinese-origin machinery carries Section 301 tariffs on top of base duty. A USA-spec panel line with 480V electricals, flying cutoff, and stacker typically runs 60,000 to 130,000 USD factory-direct, with 60 to 90 days build time plus 30 to 40 days ocean transit. Demand a full-speed factory acceptance test with your steel, and ship spare seals and shear blades in the container.

Believe Industry Company has shipped complete roll forming lines to more than 20 countries and builds US-bound machines to your inch prints — not a metric catalog.

Read the full article →

Sunday, 20 September 2026

Roll Forming Machine Guide: 5 Industries and the Process Behind Every Profile

Roll Forming Machines: One Process, Five Industries

Short answer: a roll forming machine bends a flat steel coil into a finished profile by passing it through a sequence of shaped rollers. No heat. No welding inside the forming line. One continuous process from coil to cut-to-length profile.

The full version of this topic is an 8-chapter process guide at Beli Rollforming. Here is the short version.

The process in one paragraph

The coil enters an uncoiler, passes through forming stations that bend it progressively, and exits as a finished profile cut to length in line. Gauge sets the line speed. Material behavior - work hardening, springback, coating - sets the number of stations. Get the flower pattern right and the rest follows.

Where these machines earn their keep

  • Construction - C and Z purlin lines are the most common roll forming machines sold worldwide.
  • Solar and energy - mounting rails, strut channels and brackets for ground mount and rooftop arrays.
  • Material handling - racking uprights, shelf panels and box beams for warehouse systems.
  • Electrical - cable tray and cable ladder lines, one of the fastest growing categories.
  • Roofing and cladding - standing seam, PBR, spandek and custom corrugated panels.

Why the profile list matters before the price does

The same machine family serves all five sectors, but tooling, tolerances and speeds differ between them. A buyer who fixes the profile list first avoids paying for stations that never run - and avoids discovering after commissioning that the line cannot form the profile the contract actually needs.

Read the full article: Roll Forming Machine Guide: 8 Chapters of Proven Process Knowledge

Container Roll Forming Machines: 5 Profiles, Specs and 2026 Prices

Container Roll Forming Machines: A 2026 Buyer Snapshot

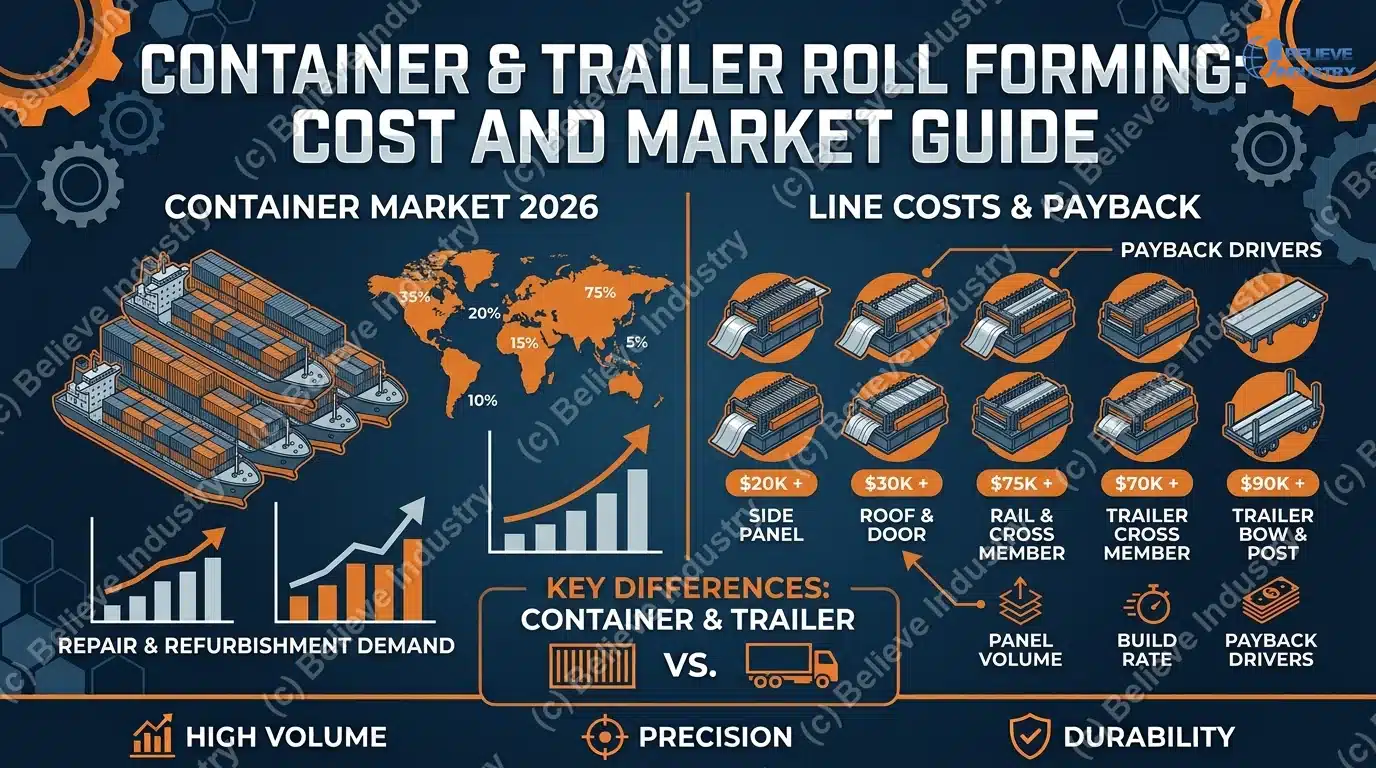
Short answer: a container roll forming machine turns Corten or high-strength steel coil into corrugated side panels, roof panels and structural rails for ISO containers and highway trailers. The line that wins is not the fastest one. It is the line that holds corrugation depth tolerance.

We just published a full buyer guide on this topic at Believe Industry Company. Here is the short version.

The 5 transport profiles

  • Container corrugated side panels - Corten A / SPA-H, 1.6-2.0 mm, 36 mm deep corrugations at 208 mm pitch, 12-20 m/min on 22-30 stands.
  • Container roof and door panels - 5 round waves, 20 mm deep, 210 mm pitch, 15-25 m/min.
  • Bottom side rails and floor cross members - about 4.5 mm SPA-H, the highest-margin profile to make in-house.
  • Trailer floor cross members and chassis side rails - Q345 / A572 Gr.50, 3.0-4.6 mm, 3-4 inch channel sections.
  • Trailer roof bows and side wall posts - Galvalume or pre-painted, 0.8-1.6 mm, up to 35 m/min, optional in-line arching station.

Why tolerance beats speed

A 36 mm corrugation depth with a plus or minus 1.5 mm tolerance is what lets a 192,000 kg stacked load pass through the corner posts. Miss the depth by 3 mm and the panel fails the vertical load test the whole container design depends on. That is the difference between transport-grade and general-grade equipment.

Price ranges at a glance

  • Container side panel lines: $180,000 to $420,000
  • Roof and door panel lines: $120,000 to $260,000
  • Bottom rail and cross member lines: $90,000 to $200,000
  • Trailer cross member and side rail lines: $110,000 to $240,000
  • Trailer roof bow and wall post lines: $70,000 to $180,000

The 2026 market angle

New container production in China dropped about 20 percent in 2025 and is forecast at 4.5 to 5 million TEU for 2026. The steady replacement cycle is now in repair, retrofit and modular conversion yards, not in new box plants. That changes which profile you should invest in first.

Read the full article: Container Roll Forming Machines - 5 Transport Profiles for 2026 for the complete spec tables, the 8-point buying checklist and the FAQ.

Believe Industry Company has built and commissioned roll forming lines in more than 20 countries for over 15 years, including container side panel, roof panel and structural lines. Every corrugation depth is profile-gauge and laser measured at three points and recorded in the FAT report.

Mining Roll Forming Machines: A Buyer's Guide to Specs, Cost, and ROI

Mining sites sit far from the nearest steel service center. A replacement bracket can take six weeks to arrive by road or barge. A fabricato...